Blog
Safety Stock: Definition, Formula, and How to Determine It
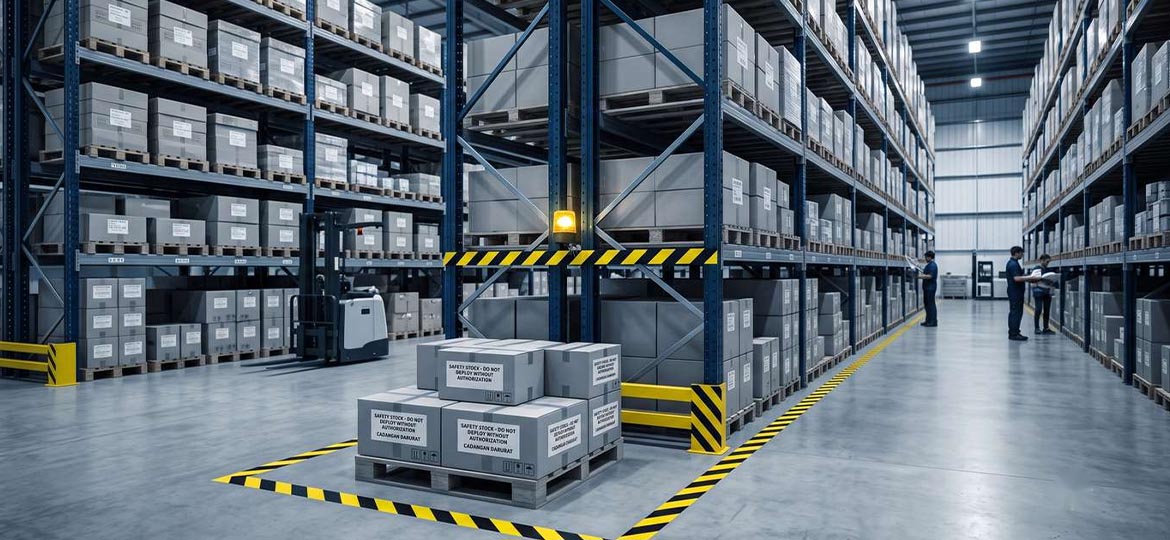
Running out of stock when demand rises is costly, and so is the capital tied up in a buffer (buffer stock) set without any calculation. Safety stock works to balance both risks. In supply chain management practice, the amount of safety stock should be calculated from data rather than guesswork. This article covers the two safety stock formulas most commonly used, worked examples of each, and the four factors that determine how large your safety stock should be.
In short, safety stock is extra inventory held above normal requirements to protect operations from uncertainty such as demand spikes, forecast errors, and supply delays. The quantity is calculated from historical sales data and lead time, allowing companies to avoid stockouts without overstocking inventory.
What Is the Safety Stock Formula?
There are two formulas commonly used by practitioners: a simple formula that compares the maximum scenario against the average, and a statistical formula based on a target service level. The choice of formula depends on data availability: the simple formula needs maximum and average figures, while the statistical formula requires enough historical data to calculate standard deviation.
|
Simple (max–average) |
(Maximum daily sales × maximum lead time) − (average daily sales × average lead time) |
Limited historical data, moderate fluctuation, a quick number is needed |
Maximum and average daily sales figures, plus lead time |
|
Statistical (service level) |
Z × σd × √lead time |
Adequate historical data, fluctuating demand, an explicit service level target |
σd (demand standard deviation), Z from the service level target, lead time |
Z is the safety factor taken from the normal distribution table according to the service level target; σd measures how far demand deviates from its average. The √lead time form is only valid when the units of σd and lead time are consistent, for example daily demand standard deviation paired with lead time in days (King, APICS magazine, 2011).
The Z-score framework assumes demand is normally distributed, a simplification that is widely accepted in practice.
Safety Stock Calculation Example
The illustration below uses the same manufacturing component scenario for both formulas. The results differ significantly: 480 units versus roughly 63 units. The gap is expected, because each formula delivers a different level of protection: one guards against the worst historical scenario, while the other aligns with a specific service certainty target.
The data: average usage of 50 units per day, maximum 70; average lead time of 10 days, maximum 14; daily σd of 12 units.
- Simple formula: (70 × 14) − (50 × 10) = 980 − 500 = 480 units.
- Statistical formula (95% service level, Z = 1.65): 1.65 × 12 × √10 ≈ 19.8 × 3.16 ≈ 63 units.
Why is the difference nearly eightfold? The simple formula combines the worst-case scenarios for both demand and lead time, so it provides maximum protection but is less efficient in terms of capital. The statistical formula only protects up to the 95% service level target; according to King, a buffer at this level still allows stockouts in roughly 5% of replenishment cycles. Safety stock is not, after all, meant to eliminate risk entirely.
This figure then becomes one of the components added together in the reorder point (ROP), the stock level that triggers a replenishment order.
How to Determine the Right Safety Stock Level
Determining safety stock is not only a matter of calculation. The formula produces a number, but the final decision is shaped by four factors: service level target, demand fluctuation, supply reliability, and holding cost. Setting a buffer based on intuition or a fixed 10–20% of cycle stock, according to King, generally delivers suboptimal performance.
- Service level target. The common standard is 95% (Z = 1.65); critical items warrant 99% (Z = 2.33). Buffer requirements rise disproportionately as the target approaches 100%, and a 100% service level is statistically unattainable; typical targets range from 90–98%.
- Demand fluctuation. The larger the standard deviation, the larger the buffer required at the same service level target.
- Supplier reliability and lead time. Supply that frequently misses schedule demands a larger buffer than a consistent supplier does.
- Holding cost. An excessive buffer locks up working capital and drives up holding costs. The right quantity is a compromise between stockout risk and cost, not simply a matter of enlarging the buffer for the sake of safety.
One prerequisite that is often overlooked is data quality. A formula is only as accurate as the data behind it. A standard deviation calculated from inaccurate stock records will produce the wrong buffer; discipline in warehouse management is the foundation of a reliable calculation.
In multi-SKU and multi-location environments, calculating parameters item by item in a spreadsheet becomes inefficient. At this stage, companies should turn to an inventory optimisation system such as SAP Integrated Business Planning (SAP IBP). The SAP IBP for Inventory module recommends safety stock across products and locations while factoring in demand variability, supply lead time variability, and service level targets (SAP Learning).
FAQ (Frequently Asked Questions)
What is the difference between safety stock and reorder point?
Safety stock is the size of the buffer stock, while the reorder point (ROP) is the stock level that triggers a replenishment order. Safety stock is one of the components added together in the ROP formula; in this article's illustration, the buffer of roughly 63 units is included in the sum when determining the reorder point.
How much safety stock is ideal?
There is no universal figure. The amount is driven by the service level target: the common 95% standard uses Z = 1.65, while critical items may go to 99% with Z = 2.33, which means a larger buffer. A 100% service level is practically impossible to reach because buffer requirements increase disproportionately.
What are the risks of holding too much safety stock?
Working capital locked up in the warehouse pushes holding costs higher. APICS/ASCM practitioners apply a rule of thumb that annual holding costs run to 15–25% of inventory value, including cost of capital, insurance, warehousing, and obsolescence. An excessive buffer directly erodes profit margins.
Conclusion
Optimal safety stock is determined from data rather than guesswork, taking into account demand variability, supply lead time, and a service level target chosen deliberately. Start with the formula that matches your data maturity, then review it whenever demand patterns shift. As an SAP Platinum Partner through its United VARs membership, Soltius implements and supports SAP supply chain planning solutions such as SAP IBP for manufacturing and distribution companies.
To discuss implementing SAP IBP in your company's inventory planning, please visit soltius.co.id.
Other News